MES ROI: where the money comes from and how to calculate the return
An MES does not pay back because it is installed. It pays back when it turns trustworthy data into decisions, and decisions into machine hours, less scrap and less manual work. This guide shows how to estimate that return with numbers that hold up in a board meeting.
Why MES ROI is so often miscalculated
Almost every MES proposal comes with a promised return. Few survive the CFO's first question: where, exactly, does this money come from? The reason is that MES ROI is indirect. The software produces nothing by itself. It measures losses accurately, shows who needs to act and supports a management routine that, month after month, recovers capacity.
When the calculation ignores that chain, it goes wrong both ways: it either promises OEE points no installation delivers on its own, or it underestimates the gain because it only looks at the license price. Three misconceptions show up often:
“The MES raises OEE”
The team raises OEE by acting on the right losses. The MES makes that possible and measurable. Without a routine, the nice dashboard becomes wallpaper.
“Every capacity gain is money”
Capacity only becomes cash if it can be sold or turned into fewer hours, less overtime or fewer shifts. Otherwise it is potential, not a result.
“The cheapest system has the best ROI”
An MES whose data nobody trusts drives no decisions. Its cost is the license plus the losses that stay invisible.
Where the money from an MES comes from
An honest business case splits the return into independent blocks, each with its own assumption and without counting the same gain twice. These are the sources that weigh most in discrete and process manufacturing plants:
Capacity recovered from OEE points
Each OEE point is output that already fit within the line's paid hours. Classified stops, micro-stops and speed loss, once visible by shift and by cause, are the losses the routine recovers first.
Machine hours freed
With higher OEE, the same output takes fewer hours. That becomes avoided overtime, cut weekend shifts, less energy and variable cost.
End of manual tracking
Operators, team leaders, supervisors and data clerks stop filling in spreadsheets and re-keying data. That time goes back to the line and to analysis.
Less scrap and rework
Deviations caught during the shift, not at the next day's audit, reduce out-of-spec output: raw material, energy and packaging that no longer go to waste.
Faster decisions
Period closing in hours, not days. Shift meetings with yesterday's data, not last month's. Hard to put a price on, but it is what makes the other blocks happen.
Postponed CAPEX
When demand grows, recovered capacity can postpone buying a new line. It goes into the business case as a scenario, not a certainty.
How to calculate MES ROI, step by step
The method below is the same one we use to build return studies with clients. It fits in a spreadsheet and can be audited line by line.
Measure the baseline OEE
Per line, not the plant average. If there is no reliable measurement, use a few weeks of records or the best data available and reflect the uncertainty in the conservative scenario.
Calculate the value of 1 point
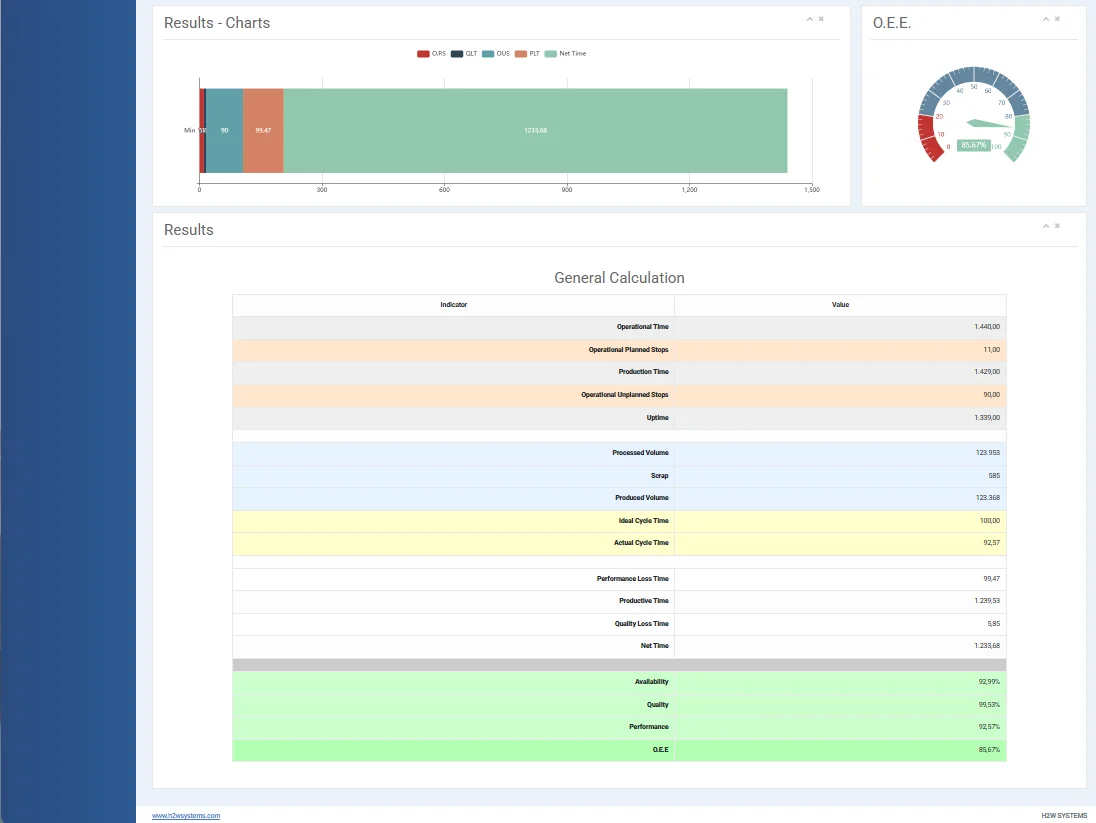
occupied hours × ideal rate × 1%That is the extra output per month in the same hours. In hours: hours × (1 − current OEE ÷ new OEE).
Set the machine-hour cost
Loaded cost: people, energy, depreciation and overhead. Then agree with the controller which share of those hours really becomes cash.
Project a realistic curve
No full gain in month 1. Spread the benefit over 3 to 24 months: first the data stabilizes, then the routine recovers the losses.
Add up every cost
Licenses or subscription, implementation, integrations and hardware, customizations, training and internal team time (key users, IT, leadership).
Close the indicators
payback · NPV · IRR · 5-year ROIWith a year-by-year cash flow and three scenarios: conservative, base and optimistic.
The gain curve: what to expect between month 3 and month 24
The most expensive mistake in a business case is putting the full gain in month 1. In practice there are three phases. In the first months, the data stabilizes: stops start being classified, the ideal rate is reviewed and the measured OEE often drops, because losses that used to be hidden come to light. Between months 3 and 12, the management routine attacks the biggest losses and the points start to climb. After that comes the mature phase, where the work is to sustain and keep improving slowly.
Dots: real H2W case results, in different plants and indicators (performance, OEE and efficiency). Dashed line: conservative curve suggested for the calculation.
The costs that belong in the calculation
Comparing only the license price skews the decision. The total cost of an MES over five years includes:
- Licenses or subscription, usually per line, per module or per user.
- Implementation: configuration, master data, calculation rules and training.
- Integrations and hardware: PLCs, sensors, shop-floor terminals, ERP interface.
- Customizations: data entry screens, reports and company-specific KPIs.
- Internal team time: key users, IT and the leadership that will run the routine. It is the most forgotten cost and the one that most shapes the result.
How much is each OEE point worth on your line?
Adjust the values to your reality. The calculator shows both sides of the same gain: hours freed (for the same output) or extra capacity (for the same hours). The starting values are those of the reference model below.
The gross ceiling assumes every freed hour becomes cash, which rarely happens. In the business case, count only the recoverable share (avoided overtime, variable cost), agreed with the controller.
What +10 OEE points do on one line
This is the reference model we use to illustrate the method, with conservative assumptions calibrated by real case gains: a line going from 55% to 65% OEE. Values are in Brazilian reais (BRL), as in the reference operation.
Look at step 7. The 92 hours would be worth over BRL 64k a month if every one became cash, but the conservative model does not count it that way. It only considers the share of hours that truly becomes savings without headcount cuts (avoided overtime and variable cost) and adds the time operators, team leaders, supervisors and data clerks no longer spend on manual records. That is why the number holds up under the finance team's review.
Add the model's third block, scrap reduction, and multiply by the plant's lines: in an operation with 30+ lines, the benefit exceeds BRL 10 million per year, with payback around 12 months.
Important: example based on the assumptions of a reference industrial operation. In each project, the calculation is redone line by line, with the plant's actual rate, baseline OEE and costs.
The mistakes that most distort MES ROI
Promising +X points just by installing
The gain comes from the routine: shift meetings, action plans, an owner for each loss. A business case that does not say who will run this is selling hope.
Ignoring demand
Extra capacity only has value if it can be sold or turned into fewer hours, less overtime or fewer shifts. State which path applies to each line.
Comparing only the license price
The license is a fraction of total cost. Implementation, integrations, customizations and internal team time weigh as much, and data quality outweighs them all.
Full gain in month 1
Measured OEE may even drop at first, when hidden losses come to light. Use a 3-to-24-month curve.
Counting the same gain twice
Hours freed and capacity sold are the same OEE point. Pick one of the two per line.
A plant-average baseline
The average hides lines at 40% and lines at 80%. The potential lies in the differences, which is why the calculation is per line.
Why a bad MES erodes ROI
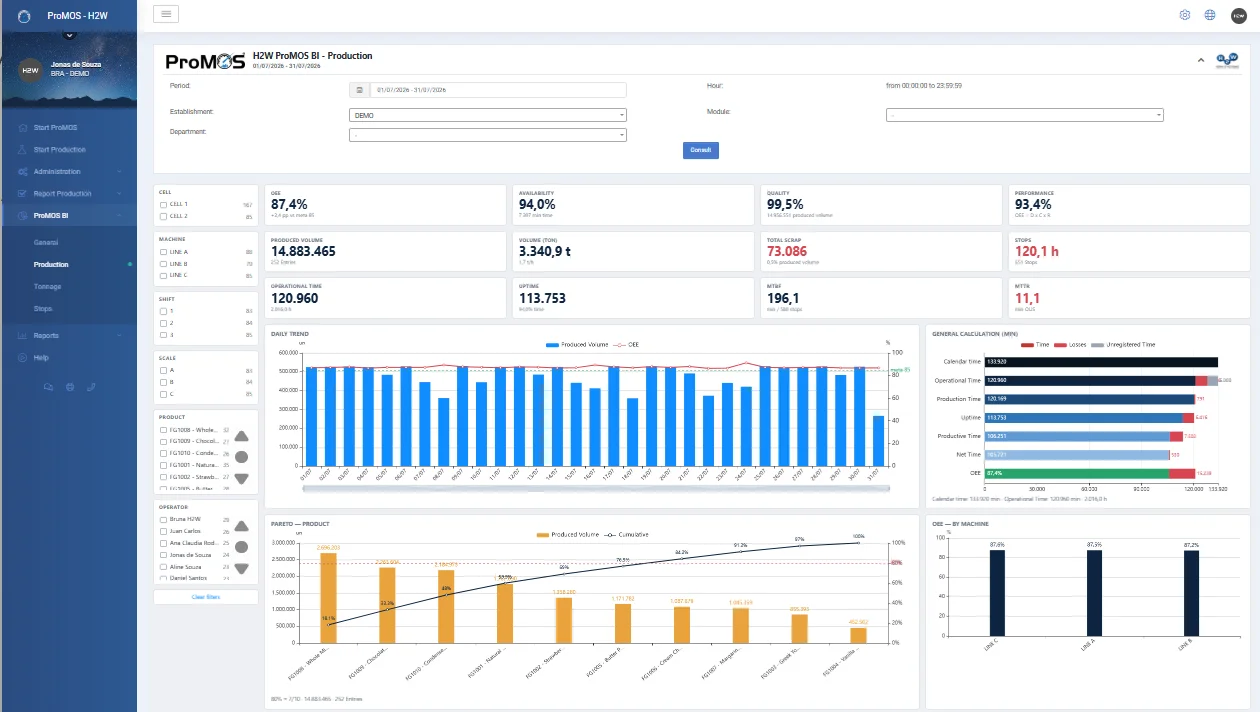
A basic machine monitor measures the machine. A real MES manages production: orders, entries by shift and operator, classified stops, OEE calculated with the company's rules, period closing and BI. The difference shows up directly in the return.
An MES that costs money
- Data nobody trusts: each department has its own number.
- The vendor's calculation rules, not the company's.
- Reports rebuilt in Excel every month-end.
- Stops with no cause, or with “other” as the cause.
- What was missed in the initial analysis never gets in: the product is closed.
An MES that pays back
- Trustworthy data, captured from the machine and validated at entry.
- OEE and KPIs calculated exactly as the company defines them.
- Reports in the format management needs, with no rework.
- Data entry screens adapted to each line's process.
- It evolves with the operation: what was missed can be added later.
That is how we build ProMOS™: a ready, proven product used by large manufacturers and, at the same time, adapted to each operation, with custom data entry, the company's exact calculations, reports the way management needs them and interfaces fitted to the process. Each client has its own environment and database. What was not foreseen in the initial analysis can be added later, without switching systems.
How to present MES ROI to the board
The board does not approve software; it approves a return with controlled risk. A presentation that works usually has these elements:
When the project goes to the board for approval, H2W builds this ROI study together with the client, using real plant data, line by line.
What the cases show
Numbers measured month by month in plants running ProMOS™, not estimates:
In all of them the pattern is the same: the return is a consequence of trustworthy data plus a management routine, not of installing software. See the cases with month-by-month data →
Questions about MES ROI
What is a typical ROI for an MES?
There is no single number: it depends on the starting OEE, the machine-hour cost, the number of lines and how much of the freed capacity turns into cash. In H2W's reference model (OEE from 55% to 65%), direct savings are about BRL 8.3k per month per line and, in an operation with more than 30 lines, the benefit exceeds BRL 10 million per year, with payback around 12 months. A serious calculation is done line by line, with real plant data.
How long does an MES take to pay back?
The first months are used to stabilize the data and build the management routine. In H2W cases, gains appeared between 3 and 12 months: +14 pp of performance in 3 months, +10 pp of OEE in 6 months and +12 pp of efficiency in 12 months. For the business case, use a conservative curve, with part of the benefit in year 1 and the full run rate from year 2 or 3.
How do I calculate the value of 1 OEE point?
Multiply the line's occupied hours by the ideal rate and by 1%: that is the extra output possible per month in the same hours. If there is no demand for that volume, convert it into hours: hours freed = occupied hours × (1 − current OEE ÷ new OEE). Then multiply by the loaded machine-hour cost, counting only the share that becomes cash (avoided overtime, variable cost).
Does an MES pay off if the plant cannot sell more?
Yes, as long as the gain is turned into fewer hours: less overtime, avoided weekend shifts, less energy and variable cost, or a postponed investment in a new line. Extra capacity is only worth money if it can be sold or turned into lower cost, and the business case must state which of the two paths will be used.
I already have an MES. Does it make sense to switch?
It makes sense when the current system does not support management: data nobody trusts, calculation rules imposed by the vendor, reports rebuilt in Excel. That MES also costs money. In a migration case from a legacy MES to ProMOS™, data reliability was kept from month 1, with no operational disruption.
Want the ROI calculated with your plant's data?
Talk to us to see ProMOS™ MES in a demo and run the numbers for your operation. If the project goes to the board, we build the full study with you, line by line.